Global fertiliser production calls for industrial components able to operate under the harshest process conditions. At Comeval Valve Systems we have answered this challenge with our latest international project in the Middle East: the supply of DN150 DIAVAL® straight-through diaphragm valves, custom designed for handling slurries and heavily contaminated fluids.
This project called for a highly engineered technological solution to transport highly concentrated phosphoric acid slurries. This critical fluid combines, in extreme form, two of the greatest threats to the service life of any installation: aggressive chemical corrosion and severe mechanical abrasion caused by the high concentration of suspended solids.
Straight-through diaphragm valves
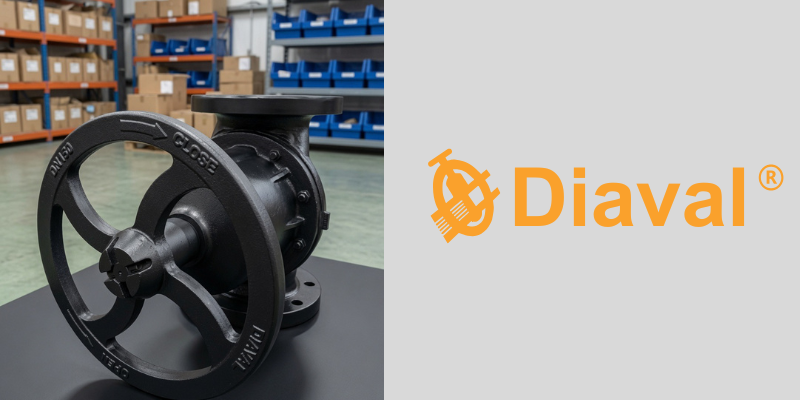
For this project, straight-through diaphragm valves are the ideal choice. Unlike weir type models, the unobstructed flow design of the straight-through series offers a fully concentric channel.
This optimised geometry brings decisive operational advantages for the fertiliser plant:
- Minimum pressure drop: the slurry moves smoothly with no internal restrictions.
- Zero blockages and sediment: its design with no internal cavities prevents phosphoric acid from building up and solidifying in the bottom of the body.
- Self-cleaning effect: when fully open, the continuous passage of the fluid itself carries the particles away, drastically reducing unplanned maintenance shutdowns.
High resistance linings and elastomers
At the heart of this project’s success lies the careful selection of materials. To withstand the simultaneous attack of abrasion and corrosion, the body of the DN150 valves has a specific, highly resistant internal lining.
This technical lining acts as an impenetrable barrier for the metal structure of the valve. Combined with the brand’s advanced elastomer diaphragms, the assembly guarantees complete tight isolation and prevents any leakage to the outside. It also allows perfect bidirectional flow shut-off and makes on-site maintenance easier without having to remove the valve from the pipeline.